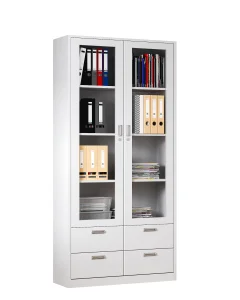
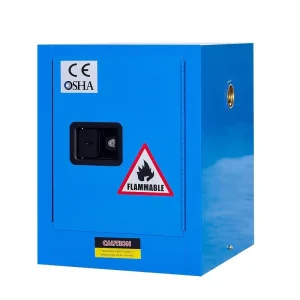
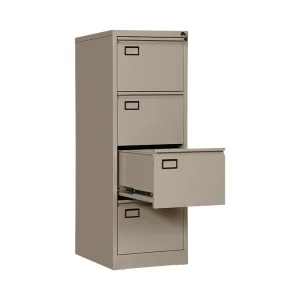
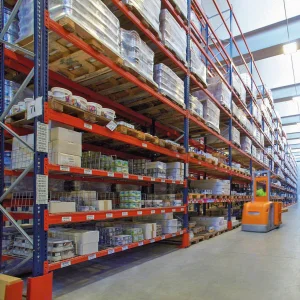
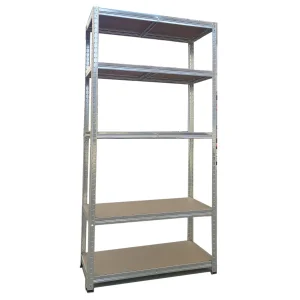
In an era of global logistics complexity, securing CE Certified Utility Storage is not just a regulatory necessity—it is a competitive advantage. As a premier manufacturer, we bridge the gap between high-capacity Chinese manufacturing prowess and the rigorous compliance requirements of the European and North American markets. Our facilities integrate advanced automation with precise engineering to deliver products that define durability and safety.
18,000㎡ of state-of-the-art production, featuring laser cutting and CNC automation.
Rigorous adherence to safety standards ensuring global market compatibility.
Strategic partnerships with 850+ top-tier vendors to ensure raw material excellence.
Our commitment to E-E-A-T is reflected in our 12+ years of industry experience. We leverage China's robust industrial supply chain to offer unmatched value, combining competitive pricing with bespoke customization.
From high-density archives in Germany to heavy-duty warehouse racking in Australia, our solutions are engineered for diverse climatic and operational environments. We specialize in seismic-resistant designs and humidity-controlled coatings essential for international infrastructure projects.
A: Yes, our products are CE certified and undergo rigorous load-capacity testing to meet international safety standards, ensuring reliability in your local warehouse.
A: Absolutely. Our R&D team of 28 engineers works closely with you to optimize your warehouse layout through tailored design software.
 Luyuan Racks